Back to Products

    ASTM A193 B7M Stud Bolts for Sour Service

    Hardness-controlled chromium-molybdenum studs tempered to 235 HBW maximum, hardness tested individually and supplied with A194 Grade 2HM nuts for wet H2S service.

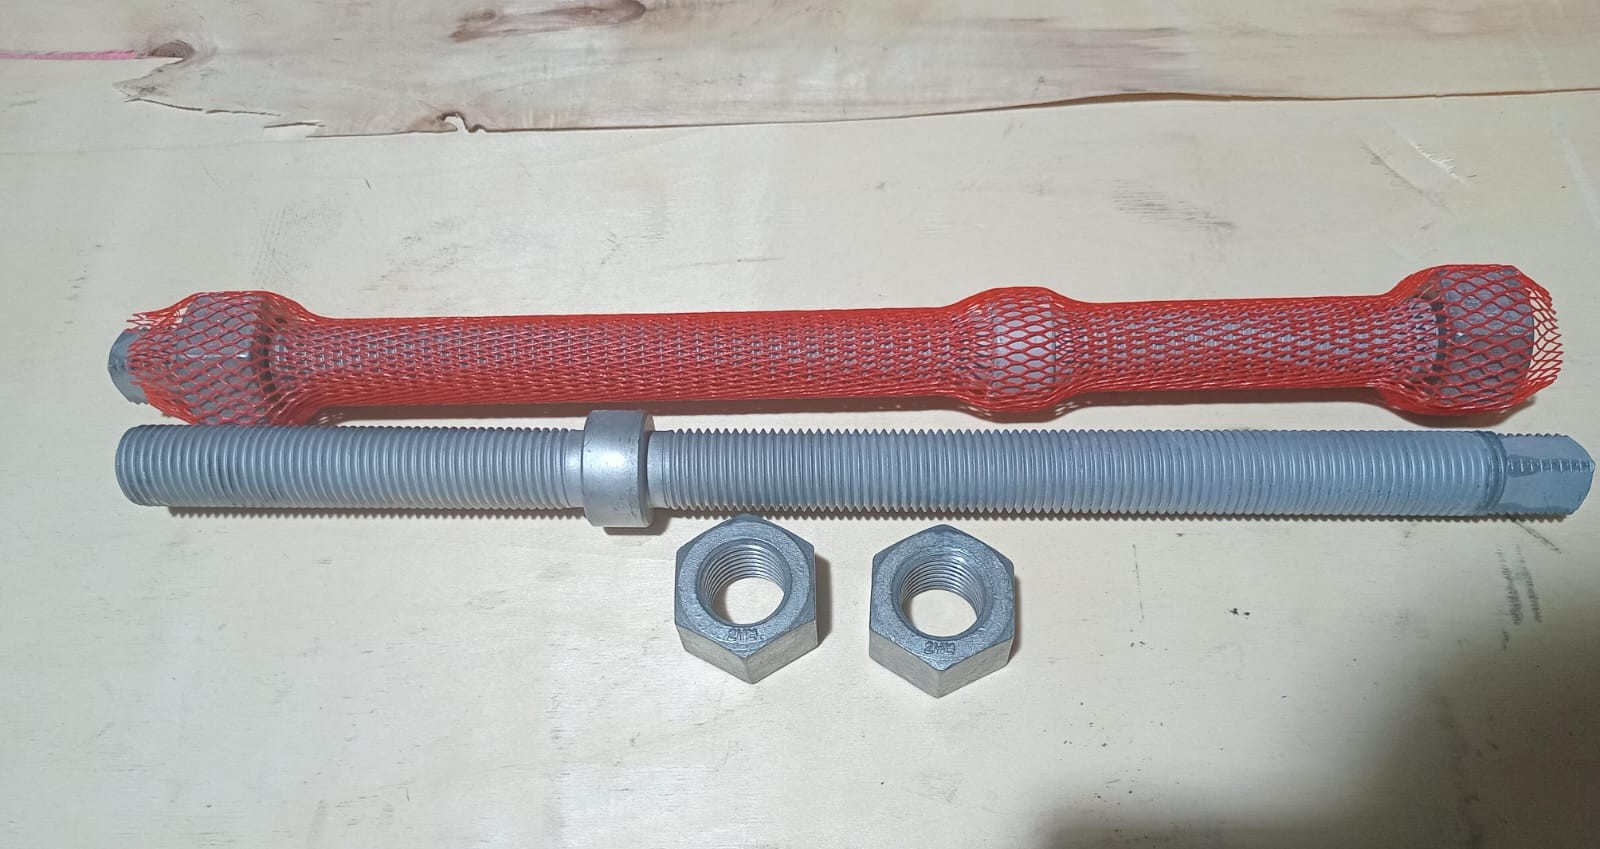
    Hot-dip galvanised ASTM A193 B7M collar bolt with two ASTM A194 2HM heavy hex nuts
    Made-to-drawing B7M collar bolt with A194 2HM nuts, hot-dip galvanised and mesh sleeved
    EN 10204 3.1 Certified
    ISO 9001 Quality
    ASTM A193 B7M collar bolts in protective mesh sleeves with galvanised 2HM nuts
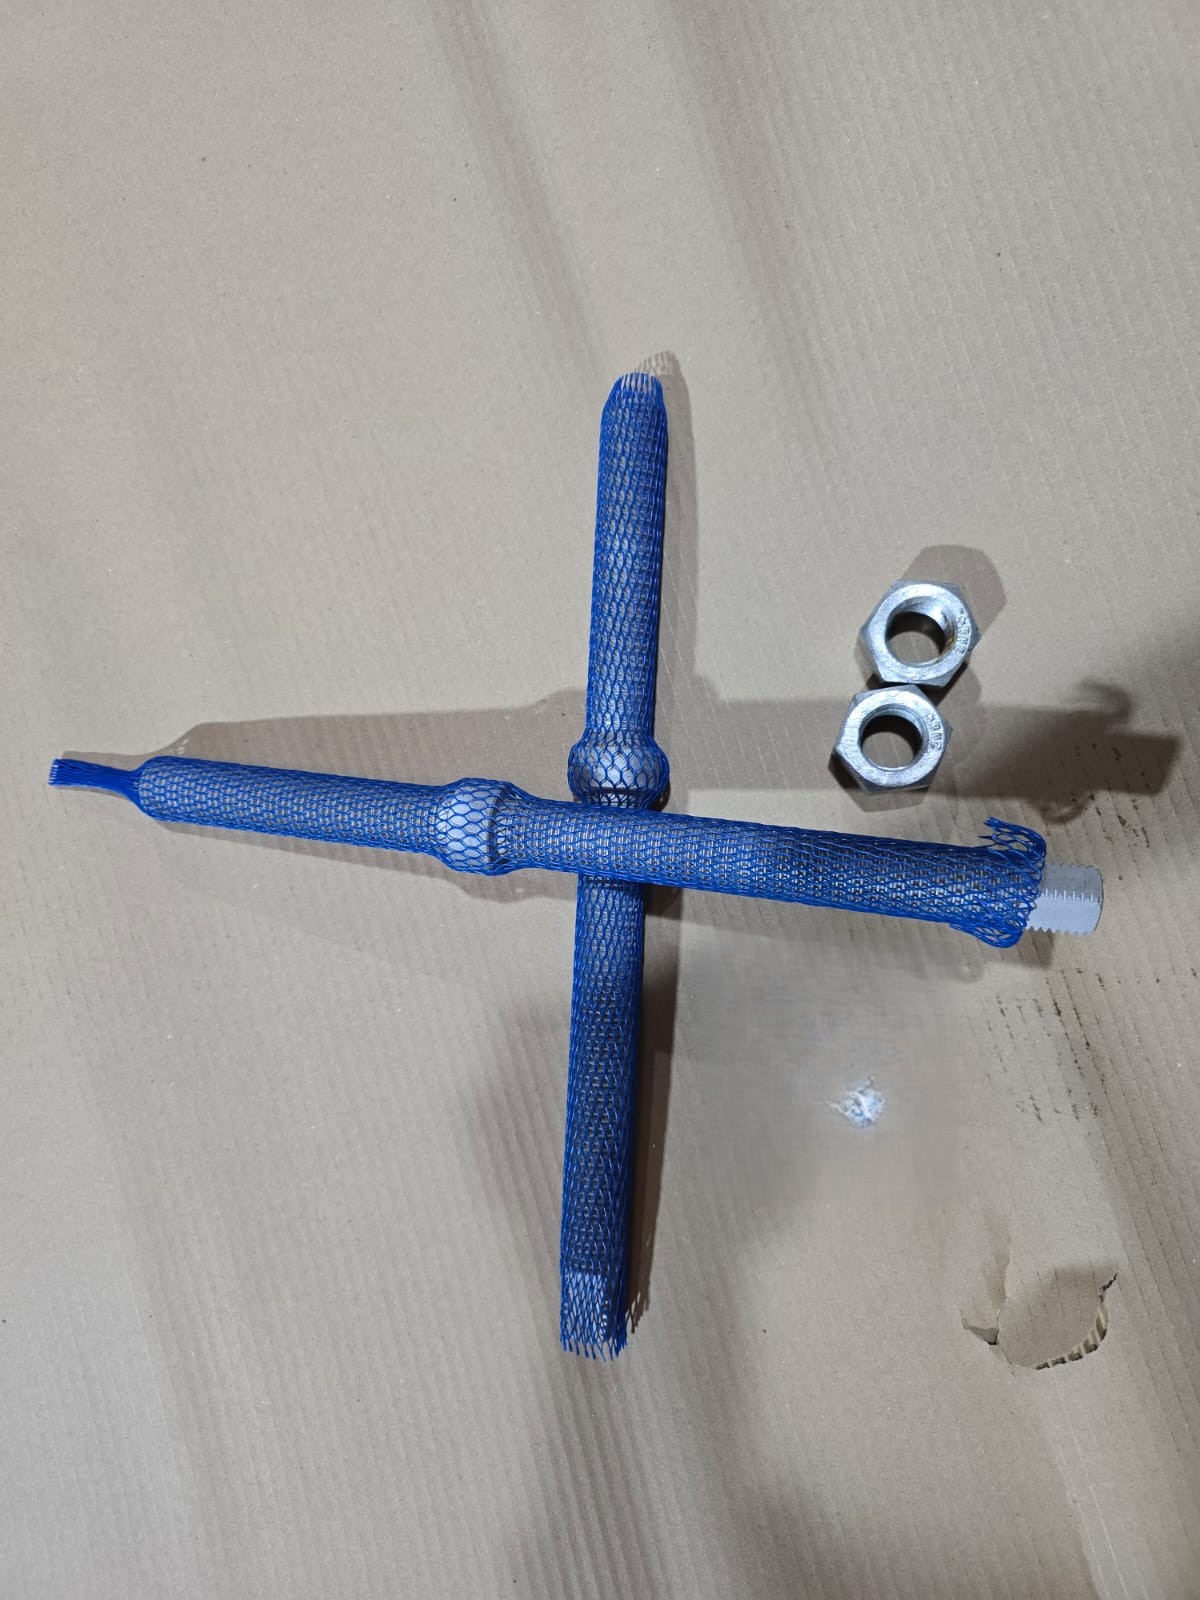
    B7M collar bolts individually sleeved for damage-free site handover

    Overview

    ASTM A193 Grade B7M is the sour service variant of B7. It uses the same AISI 4140 chromium-molybdenum chemistry but is tempered at a higher temperature to bring hardness down to a maximum of 235 HBW (99 HRB), which is the threshold NACE MR0175 / ISO 15156 sets for resistance to sulphide stress cracking in wet H2S environments. The trade-off is strength: minimum tensile drops to 689 MPa (100 ksi) and minimum yield to 551 MPa (80 ksi), so bolt loads and joint calculations must be revisited rather than carried over from a B7 design. Every B7M stud EMG supplies is hardness tested individually, not by batch sample, and the readings appear on the EN 10204 3.1 certificate.

    B7M is not simply a softer B7 — it is individually hardness tested to a 235 HBW maximum and paired with A194 2HM nuts, because in wet H2S service a single over-hard component is enough to initiate sulphide stress cracking.

    Typical Applications

    • Wellhead and Christmas tree flange bolting in sour gas fields
    • Sour service process piping and separator vessel closures
    • Amine, sulphur recovery and gas sweetening unit bolting
    • Subsea and topside connections handling H2S-bearing fluids
    • Sour crude pipeline valve and pig trap assemblies
    • Upgrades where existing B7 bolting no longer meets a reclassified sour envelope

    B7M Configurations We Supply

    • Continuous thread B7M studs cut to project length
    • Double-end B7M studs with defined grip length
    • Complete B7M/2HM kits with two hardness-tested heavy hex nuts
    • B7M kits with coating applied to the nominated customer specification
    • Hardness-mapped studs with individual readings recorded per piece

    Common Materials & Grades

    ASTM A193 B7MAISI 4140 / 42CrMo4ASTM A194 2HM nutsASTM A320 L7MDuplex 2205Inconel 718

    Standards & Documentation

    • ASTM A193/A193M Grade B7M including the mandatory hardness testing requirement
    • NACE MR0175 / ISO 15156 for materials in H2S-containing oilfield environments
    • ASTM A194 Grade 2HM for the mating nuts, also hardness controlled
    • EN 10204 3.1 mill test reports with individual hardness readings recorded
    • Heat number traceability through tempering, machining and coating
    • EN 10204 3.2 third-party witnessed certification available on request

    NEED MACHINED COMPONENTS TOO?

    Spacers, blinds, special nuts, shafts and bushes — supplied to your drawing with the same traceability as your bolting. Precision Machined Components →

    Why hardness, not strength, is the controlling property

    Sulphide stress cracking is a hydrogen-assisted mechanism. Atomic hydrogen generated by corrosion in a wet H2S environment enters the steel and embrittles the microstructure, and susceptibility rises sharply with hardness. NACE MR0175 / ISO 15156 therefore caps carbon and low alloy steel bolting at 235 HBW rather than setting a strength ceiling. B7M meets that cap by tempering at a minimum 620 C. This is also why substitution is dangerous in the other direction: a B7 stud installed into a sour joint will pass every strength check and still crack in service, sometimes within months.

    Testing regime that separates B7M from B7

    ASTM A193 requires B7M to be hardness tested on 100 percent of production studs after final heat treatment, with the test taken on the end or a machined flat, and every reading must fall within the acceptance band. Nuts to A194 2HM carry the same individual testing obligation. EMG records the readings against piece and heat number so a client auditing a sour joint can trace an individual stud back to its tested hardness rather than to a batch average, which is the level of evidence operators and certifying authorities increasingly ask for during sour reclassification work.

    Redesigning the joint for lower bolt load

    Moving a joint from B7 to B7M reduces allowable bolt stress by roughly 20 percent. On a gasketed flange that can mean the seating stress the gasket needs is no longer achievable at the same bolt count and diameter, so the joint may need a softer gasket, a larger stud diameter, or a change of gasket style. This is worth resolving before the bolting is ordered. Send us the flange rating, gasket type and design conditions with the enquiry and we will flag where the substitution changes the assembly.

    Coating in sour service

    Coating selection on sour service bolting is strictly customer specified. Processes that risk introducing hydrogen — notably electroplating — are generally excluded in favour of mechanically applied or dip-spin systems. Fluoropolymer and zinc-flake systems are widely nominated because they combine corrosion protection with predictable friction for torque control. EMG applies only the system named in the specification and supplies the applicator certificate with the documentation pack.

    FREQUENTLY ASKED QUESTIONS

    Technical FAQs

    What is the difference between ASTM A193 B7 and B7M?

    +
    Same chemistry, different heat treatment and testing. B7M is tempered higher to hold hardness at 235 HBW maximum for sour service compliance, which lowers minimum tensile from 862 to 689 MPa and minimum yield from 724 to 551 MPa. B7M also requires 100 percent hardness testing, where B7 does not.

    Is B7M automatically NACE MR0175 compliant?

    +
    B7M is the grade NACE MR0175 / ISO 15156 recognises for carbon and low alloy steel bolting exposed to wet H2S, provided the hardness limit is verified and documented. Compliance is a documentation outcome as much as a material one, so we supply the individual hardness readings and heat traceability that an audit requires.

    Which nuts must be used with B7M studs?

    +
    ASTM A194 Grade 2HM. Standard 2H nuts are not hardness controlled to the sour service limit and must not be substituted, even temporarily during a shutdown.

    Can B7M be used for exposed atmospheric bolting?

    +
    Yes, and it is common on sour facilities to standardise on B7M to eliminate the risk of mixed bolting on site. It needs corrosion protection in the same way B7 does, and the lower strength must be accounted for in the joint calculation.

    Do you supply B7M studs with 3.2 certification?

    +
    Yes. EN 10204 3.2 third-party witnessed certification is available, including inspection by the client's nominated authority. Nominate the inspection body at enquiry stage so the witness points can be scheduled into manufacture.

    What is the maximum diameter available in B7M?

    +
    We supply B7M from 1/4in to 6in and M5 to M150 as standard, with larger diameters quoted per project. Large-diameter sour service studs may need forged bar and a longer tempering cycle, which affects lead time.
    GET IN TOUCH

    Need a Quote for ASTM A193 B7M Stud Bolts?

    Send us the size, grade and quantity — or your drawings and bill of materials — and we'll return a technical quote for astm a193 b7m stud bolts with lead times and certification included.

    Emergency Support

    24/7 availability for critical projects