Back to Products

    Petrochemical Stud Bolts for Perth & Western Australian Process Plants

    Certified ASTM A193 B7, B7M, B8M, super duplex and nickel alloy stud bolt kits supplied to Perth, Kwinana, Karratha and the Pilbara — coated to specification, bagged per joint and covered by EN 10204 3.1 certification.

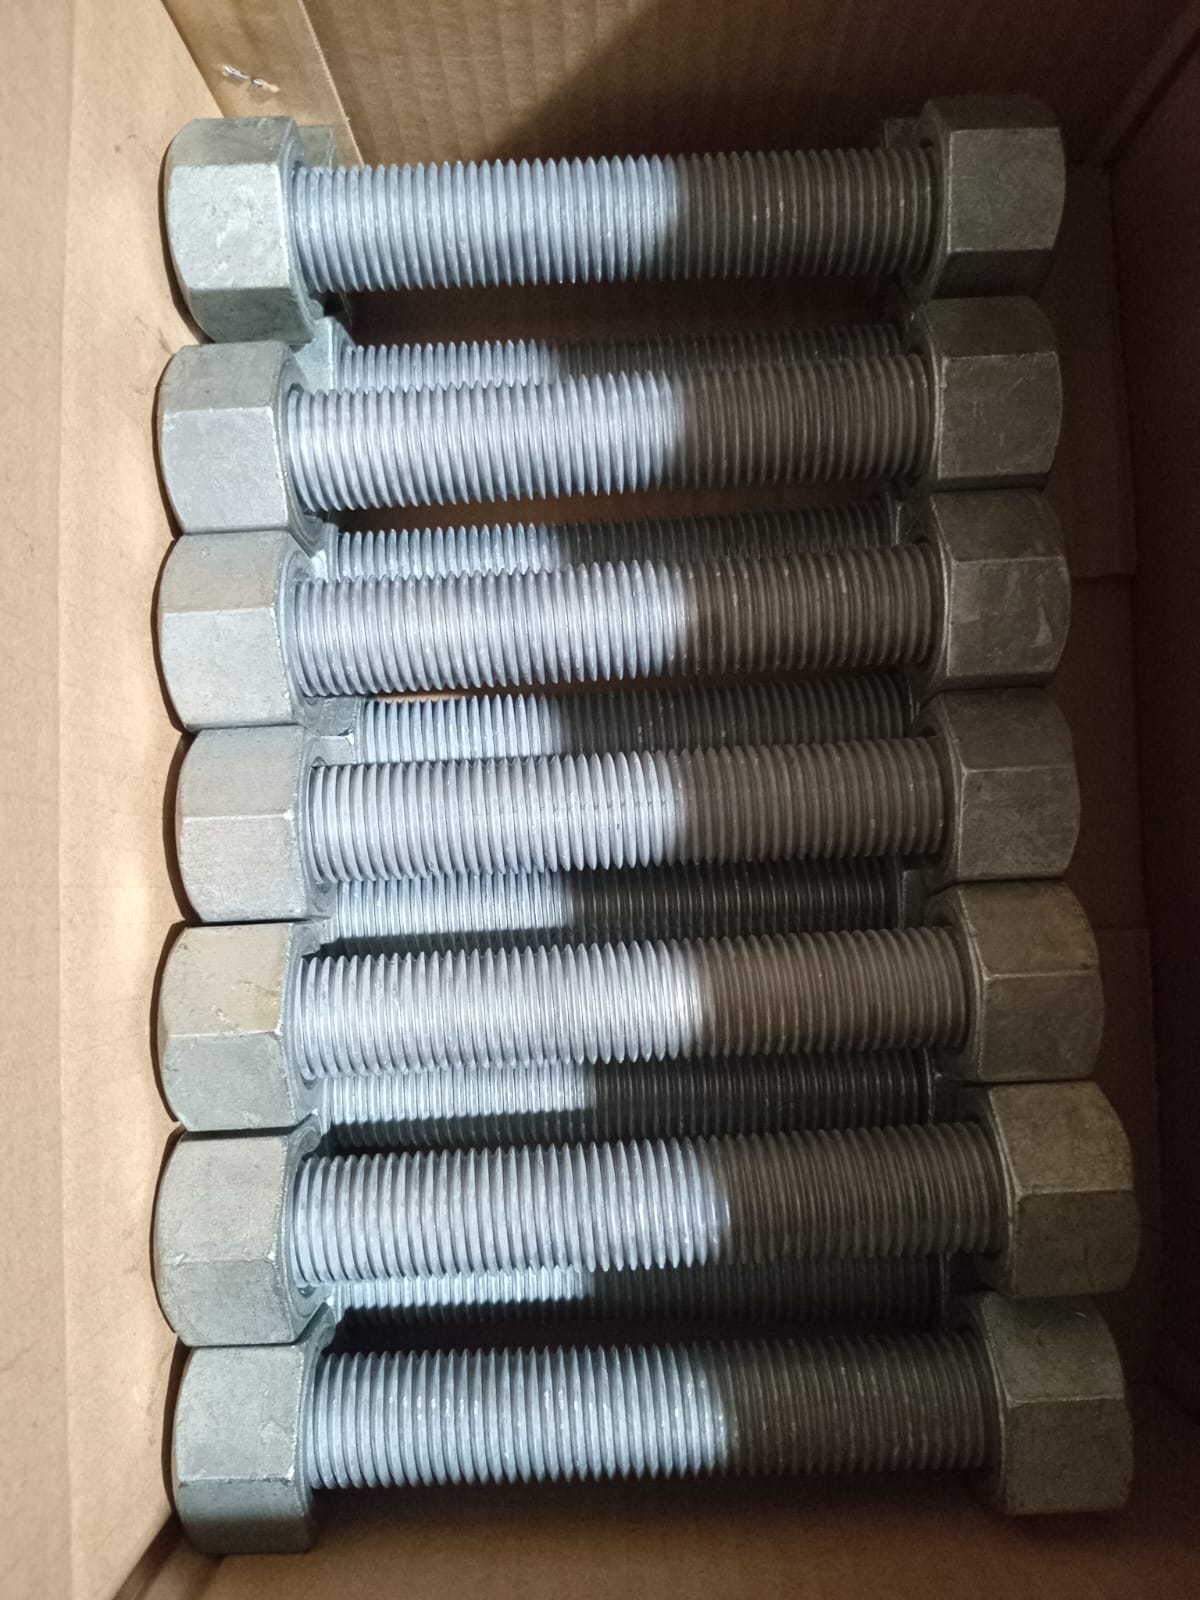
    Hot-dip galvanised ASTM A193 B7 petrochemical stud bolts with A194 2H heavy hex nuts for Perth refinery bolting
    A193 B7 / A194 2H petrochemical stud bolt kits supplied into Western Australia
    EN 10204 3.1 Certified
    ISO 9001 Quality
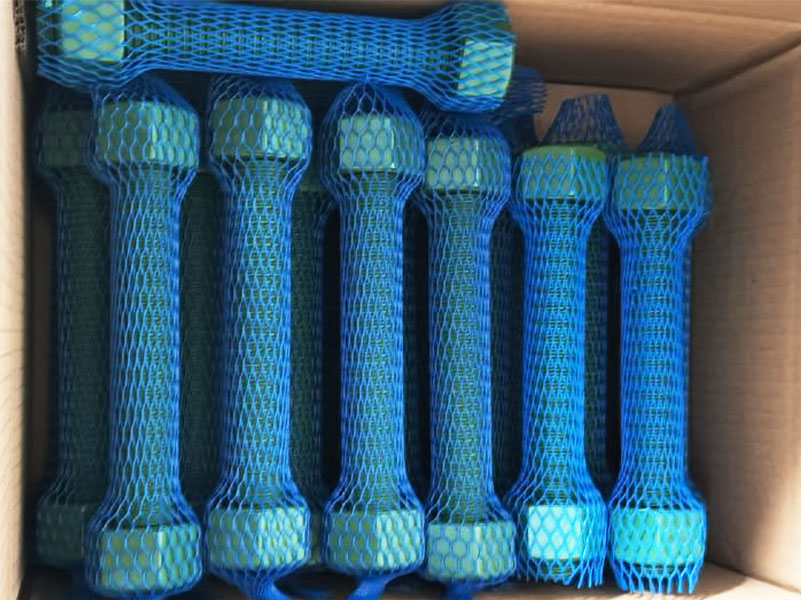
    Xylan 1424 coated petrochemical stud bolts for chloride-exposed WA process piping
    Xylan 1424 coated studs for coastal and chloride-heavy WA service

    Overview

    Petrochemical bolting in Western Australia is a corrosion and certification problem before it is a supply problem. Kwinana refining and chemical plants, Burrup fertiliser and ammonia trains, North West Shelf and Pilbara LNG facilities, and the alumina refineries along the coast all combine hot process duty with salt-laden air and long shutdown intervals. Energy Materials Group supplies Perth and WA engineering houses, EPCs, shutdown contractors and asset owners with petrochemical stud bolts specified to the joint — ASTM A193 B7 for standard high-temperature flange duty, B7M where NACE MR0175 / ISO 15156 sour service applies, B8M Class 2 for chloride and produced-water exposure, and super duplex UNS S32750/S32760 or Inconel 718/725 where seawater, subsea or high-temperature service rules anything less out. Every kit ships with EN 10204 3.1 mill certification and heat-number traceability, with 3.2 third-party inspection available on request.

    Energy Materials Group supplies petrochemical stud bolts to Perth, Kwinana, Karratha and the Pilbara as complete kits — stud, two ASTM A194 2H nuts, optional F436 washers — coated to specification, bagged and tagged per flange, with EN 10204 3.1 certification issued ahead of the goods.

    Typical Applications

    • Kwinana refinery and chemical plant flange bolting on process piping
    • Burrup ammonia, fertiliser and methanol train shutdown bolting
    • North West Shelf and Pilbara LNG trains, tie-ins and compressor casings
    • Alumina refinery digestion, evaporation and slurry line joints
    • Pressure vessel manways, blind flanges and heat exchanger closures
    • Kwinana and Karratha desalination and seawater intake bolting

    Petrochemical Bolting We Supply into WA

    • ASTM A193 B7 / A194 2H petrochemical stud bolt kits, 1/4in to 6in and M5 to M150
    • ASTM A193 B7M / A194 2HM hardness-controlled kits for sour service
    • ASTM A193 B8M Class 2 / A194 8M kits for chloride and CRA flanges
    • ASTM A320 L7 / L7M kits for cryogenic and low-temperature LNG duty
    • Super duplex UNS S32750 / S32760 studs for seawater and produced water
    • Inconel 718 / 725, Incoloy 825 and Monel K-500 studs for subsea and high-temperature joints

    Common Materials & Grades

    Standards & Documentation

    • EN 10204 3.1 mill test reports with chemistry, mechanical properties and heat treatment
    • EN 10204 3.2 third-party inspected certification on request
    • NACE MR0175 / ISO 15156 hardness compliance for sour service bolting
    • Coating applicator certificates for Xylan 1424, GEOMET 321/500, PTFE and HDG to AS/NZS 4680
    • Thread inspection to ASME B1.1 Class 2A or ISO 261/965
    • ISO 9001:2015 certified quality management and heat-number traceability

    NEED MACHINED COMPONENTS TOO?

    Spacers, blinds, special nuts, shafts and bushes — supplied to your drawing with the same traceability as your bolting. Precision Machined Components →

    Which grade suits a Perth or Pilbara petrochemical joint

    For a standard hydrocarbon process flange operating above ambient, ASTM A193 B7 with A194 2H nuts remains the default and is what most Kwinana and Burrup specifications call up. The moment wet H2S enters the stream, hardness-controlled B7M with 2HM nuts is mandatory under NACE MR0175 / ISO 15156 — substituting B7 is a compliance failure, not a preference. Below minus 29 C, as on LNG and cryogenic service across the North West Shelf, ASTM A320 L7 or L7M applies because it is impact tested. Where sustained metal temperature climbs past roughly 500 C, B16 takes over. On seawater, produced water and desalination duty, or where the flange itself is a corrosion-resistant alloy, B8M Class 2, super duplex or a nickel alloy avoids galvanic and chloride pitting problems that will otherwise seize the joint before the next turnaround.

    Coatings for coastal Western Australian exposure

    Perth's coastal strip, the Burrup Peninsula and the Pilbara ports all deliver chloride-laden air and cyclonic wet seasons. Plain black B7 will scale within a maintenance cycle in that environment, so most WA petrochemical specifications nominate a coating. Xylan 1424 gives a low, repeatable friction coefficient that suits torque-controlled tightening and prevents disassembly seizure at the next shutdown. GEOMET 321 and 500 provide sacrificial zinc-flake protection without hydrogen embrittlement risk on higher-strength grades. Hot-dip galvanising to AS/NZS 4680 remains common on structural and onshore utility bolting but changes thread clearance and torque behaviour, so it must be nominated before torque figures are issued. We apply coatings strictly to specification and include the applicator certificate in the documentation pack.

    Freight, lead times and shutdown response into WA

    Stock and mill-direct orders consolidate through our Brisbane hub and move to Perth, Kwinana, Karratha, Dampier and Port Hedland on scheduled air and road freight, delivered direct to site or to your nominated forwarder. Common sizes in standard ASME B16.5 flange lengths ship within days. Non-standard lengths, coated kits, sour-service testing scopes and large diameters typically run three to six weeks depending on coating and inspection requirements. Documentation is issued ahead of the goods so QA sign-off is not the thing holding up a turnaround, and breakdown or unplanned shutdown requirements are handled through RapidBolt, our 24/7 emergency bolting response.

    Kits packed to the joint list, not to a box count

    A Pilbara or Kwinana turnaround loses hours when crews sort loose studs and nuts on the deck. We supply petrochemical stud bolts as complete kits — stud, two heavy hex nuts, optional ASTM F436 hardened washers — with the nut heat matched to the stud heat so a single EN 10204 3.1 certificate covers the assembly. Where a joint list is provided, kits are bagged, tagged and labelled per flange tag number so each bag goes straight to the joint. That packaging discipline is what separates engineered supply from an off-the-shelf order, and it is the single biggest schedule saver on a WA shutdown.

    FREQUENTLY ASKED QUESTIONS

    Technical FAQs

    Do you supply petrochemical stud bolts in Perth?

    +
    Yes. Energy Materials Group supplies petrochemical stud bolts and complete bolting kits into Perth, Kwinana, Henderson, Karratha, Dampier, Port Hedland and Bunbury, delivered direct to site or to your nominated freight forwarder. Contact sales@energymaterialsgroup.com or call +61 7 4055 6928 with your joint list or flange schedule.

    Which stud bolt grade do WA refineries and LNG plants usually specify?

    +
    ASTM A193 B7 with A194 2H nuts is the default for standard high-temperature hydrocarbon flange duty. B7M with 2HM nuts is specified where NACE MR0175 / ISO 15156 sour service applies, A320 L7 for cryogenic LNG service, and B8M Class 2, super duplex or Inconel where chloride, seawater or subsea exposure rules out alloy steel.

    What coating should petrochemical stud bolts have for coastal WA service?

    +
    Xylan 1424 is the most common choice for Perth and Pilbara process bolting because it combines corrosion protection with a low, repeatable friction coefficient for torque-controlled tightening. GEOMET 321/500 suits higher-strength grades where hydrogen embrittlement is a concern, and hot-dip galvanising to AS/NZS 4680 is used on structural and onshore utility bolting.

    What certification is supplied with WA petrochemical bolting?

    +
    EN 10204 3.1 mill test reports covering chemistry, mechanical properties and heat treatment, with full heat-number traceability. EN 10204 3.2 third-party inspected certification, PMI, hardness verification and coating applicator certificates are available where the project specification requires them.

    How fast can stud bolts reach a Karratha or Kwinana shutdown?

    +
    Common sizes in standard flange lengths ship from Australian stock within days on air or road freight. Non-standard lengths and coated or specially tested kits generally run three to six weeks. Unplanned breakdowns and emergency shutdown requirements are handled through RapidBolt, our 24/7 emergency bolting service.

    Do you supply general trade or automotive fasteners in Perth?

    +
    No. We supply engineered, certified bolting for petrochemical, LNG, mining and industrial projects on a project and shutdown basis only. We do not supply retail, automotive or general hardware fasteners.
    GET IN TOUCH

    Need a Quote for Petrochemical Stud Bolts Perth?

    Send us the size, grade and quantity — or your drawings and bill of materials — and we'll return a technical quote for petrochemical stud bolts perth with lead times and certification included.

    Emergency Support

    24/7 availability for critical projects